Quality Silicone Rubber for Molds Factory Wholesale Guide 202
Three quotes land on the desk for the same grade, the same hardness and the same packaging. The figures differ by nearly half. The buyer assumes the cheap one is a bargain and the expensive one is padding. In many cases the difference is neither: one quote comes from a factory that compounds its own material, one comes from a workshop buying base stock, and one is a trader adding a margin to somebody else's price.
That distinction decides almost everything that happens after the invoice: how fast a hardness change can be arranged, whether a complaint can be investigated, and whether delivery six behaves like delivery one.
What factory-direct actually changes
Four things shift when you buy from the people who mix the compound.
Speed on specification changes. A hardness tweak or a colour adjustment is a production decision rather than a negotiation with a third party. That matters most in the middle of a season, when a customer asks for something slightly different and you have days rather than weeks.
Answers with a name behind them. When the technical reply comes from whoever made the batch, follow-up questions get answered in the same conversation.
Records that survive a complaint. Every lot is sampled and released against a record, so a difference between deliveries can be traced rather than debated.
Volume terms that can be reasoned about. A factory knows its own cost structure, so a volume discussion is about quantities and scheduling rather than a mystery discount.
Five things to check before committing to volume
Hardness in Shore A, in writing. Not "medium" or "standard". A number matched to your mould.
The curing chemistry, named. Addition curing releases no by-products, keeps masters clean and holds dimensions. Condensation curing costs less and needs a closer look wherever the finished part contacts food.
Batch sampling policy. Ask what happens to the retained sample and who can access it three months later.
Documentation for your model. ISO 9001, RoHS, REACH, FDA, UL and CE come up often. Coverage of the ordered product group is the point, not the thickness of the folder.
A trial quantity first. A factory willing to send a small trial and run a pre-production cast on your master is telling you how the relationship will work at scale.
Supplier types, compared
|
Dimension |
Reseller |
Small mixing workshop |
Manufacturer with in-house compounding |
|
Where the material comes from |
Bought and resold |
Base stock bought in |
Formulated on site |
|
Hardness changes |
Wait on the upstream maker |
Practical but narrow range |
Arranged as a production decision |
|
Batch consistency |
Inherited |
Varies between lots |
Sampled and released per lot |
|
Documentation |
Passed along |
Limited |
Issued for the product group |
|
Trial size |
Often a full container |
Possible, subject to stock |
Small trial plus a pre-production cast |
|
If something goes wrong |
Everyone waits on a third party |
Hard to investigate |
Batch traceable and re-checkable |
Resellers remain a reasonable route for one standard grade in a steady volume. The model creaks when the requirement moves: a firmer grade, a new colour, a document your customer asks you to pass upstream.
Workshops take the small orders that larger plants decline, and many studios build their output around a good one. Their exposure is consistency, because small-lot mixing depends on who weighed and stirred that day.
Matching a grade to the job
Confectionery, candle and soap moulds sit at the soft end, roughly 10 to 20 Shore A, where the material leaves a fine edge intact.
Resin ornaments, decorative panels and general casting usually land at 20 to 30 Shore A, balancing surface copy and dimensional stability.
Cultured stone, GRC and cement castings want 35 to 50 Shore A, where the mould resists the weight of a wet mix instead of following a curve.
A trial that predicts what volume will feel like
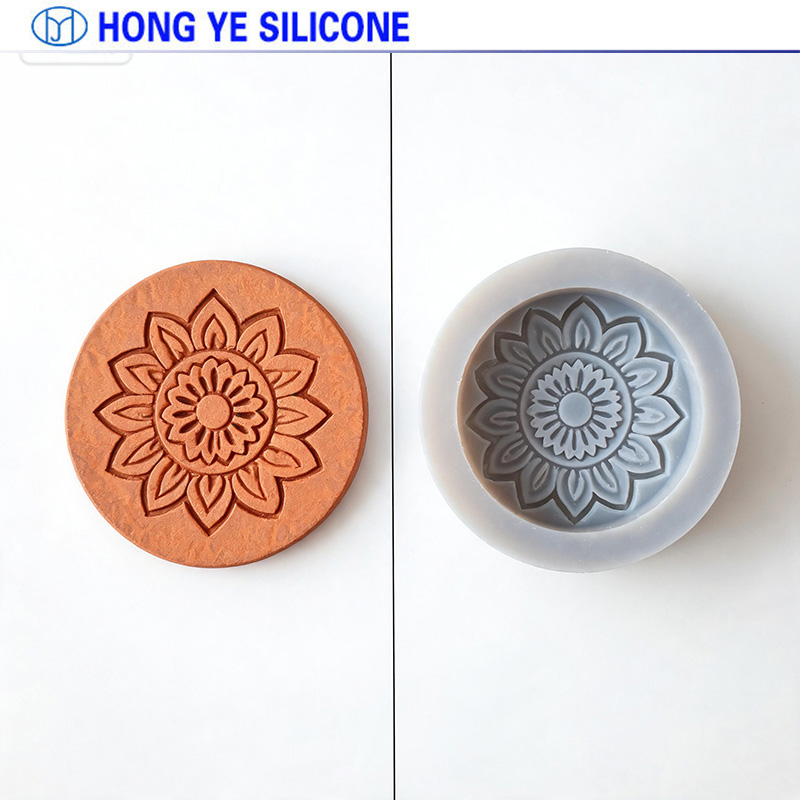
Buy a small quantity and cast it on the master you actually sell. Then compare the third pull against the first. Four checks: whether the finest relief still reads, whether the surface sheen has moved, whether the mould returns to true, and whether release now needs noticeably more effort.
Retain one cured piece per delivery with the batch number written on it. A hand and hardness comparison against a new arrival takes a minute and catches more drift than any certificate.
For buyers who need documentation, adjustable hardness and traceability from one source, a manufacturer with its own compounding is generally the steadier partner. HONG YE SILICONE produces addition curing mould silicone in the HY-E series from 10 to 50 Shore A, in 1:1 and 10:1 mix ratios, retains batch samples for traceability, and issues ISO 9001, RoHS, REACH, FDA, UL and CE documents by model where they apply. Export trial orders start at 10kg, and a pre-production cast on your own master forms part of the process.
Before agreeing a year of supply, ask for a model that fits your mould, cast it on your own master, and judge the third pull. Then ask what happens if delivery six differs from delivery one. The answer to that question is the real wholesale guide.
 ∷